Thread Repair with HeliCoil Inserts
Sep 18, 2026
Repairing threads
Normally, if the hole diameter has not been enlarged substantially, we can simply re-thread (or re-tap) the hole using cutting taps. However, when thread damage causes the hole to become oversized such that the original bolt or screw cannot be used, we will then need to move on to thread repair with the aid of threaded inserts.
Section A: Introduction to Screw Thread Inserts
A thread insert is broadly defined as a part that can be inserted into the hole of the work piece as a separate thread media. They act as a means of compensating for the increase in the hole diameter while returning it to its original size. Thread inserts usually have high quality wear resistance and shear strength in relation to the parent material. As such, most of them are made of stainless steel, even though you may find a diverse range of materials from Carbon Steel, Inconel, Bronze to Nitronic-60.
In the fastening industry, there are a wide range of thread inserts. All of them differ in terms of cost, application and design, among other factors. In this manual, we will look at HeliCoil inserts, which is widely considered to be the original screw thread insert.
Section B: HeliCoil Screw Thread Insert
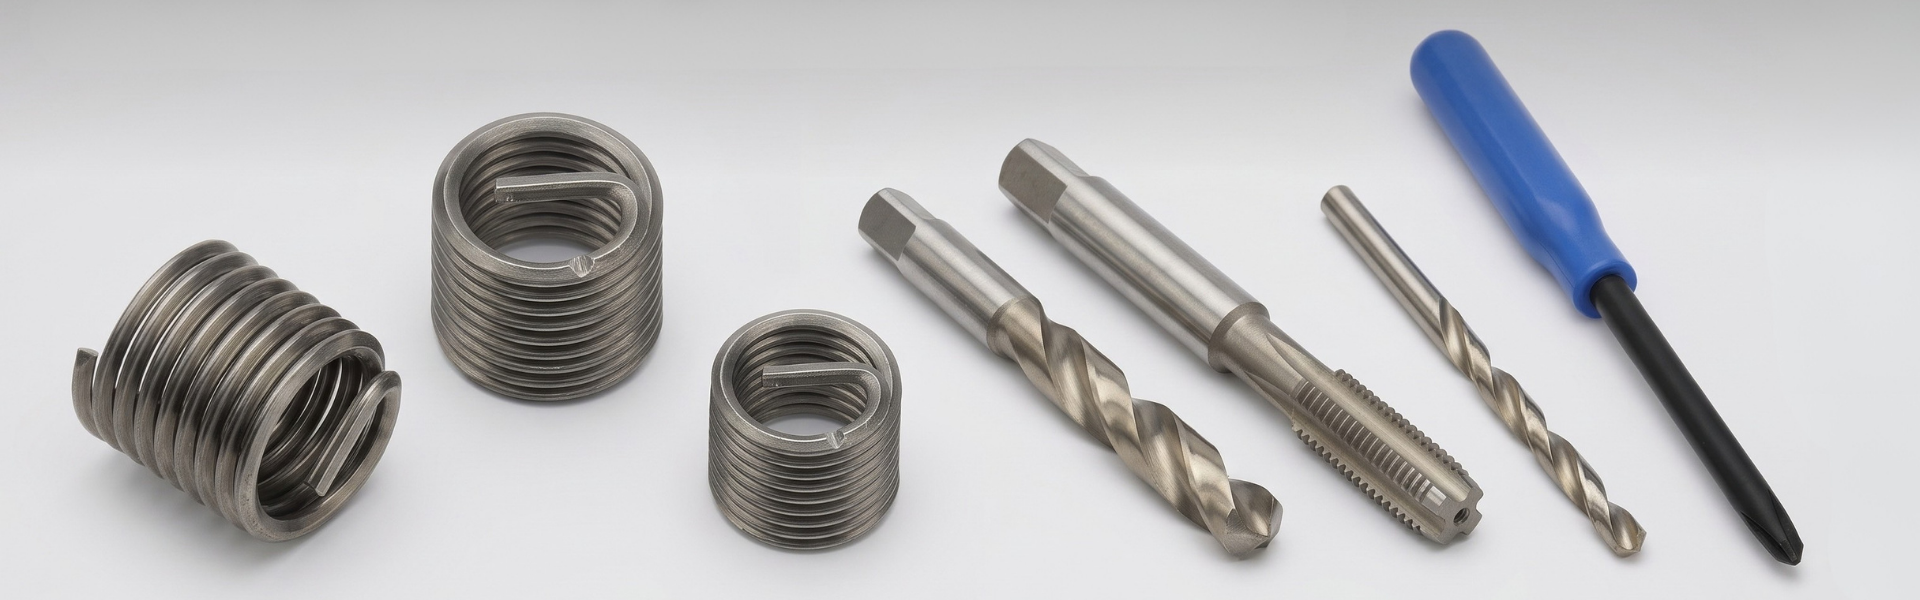
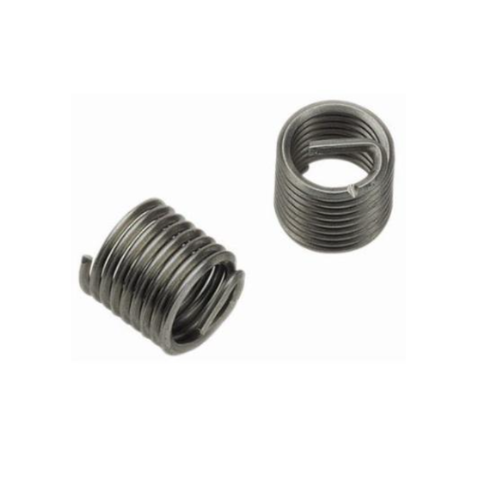
HeliCoil inserts have a spring-like appearance with a diamond (or rhombus) cross-section. After installation, they act as an internal thread in the work piece. As they have stronger shear strength with relation to the parent material, they are the point of contact that the fastening screw will have to the work piece, thus providing it protection from wear and tear.
They protect tapped threads against failures due to stripping, seizing, corrosion and wear. Due to their flexibility, helical inserts create internal threads which have a much improved distribution of residual stress loading when compared with conventional tapped holes.
Section C: HeliCoil Thread Insert Repair Tools
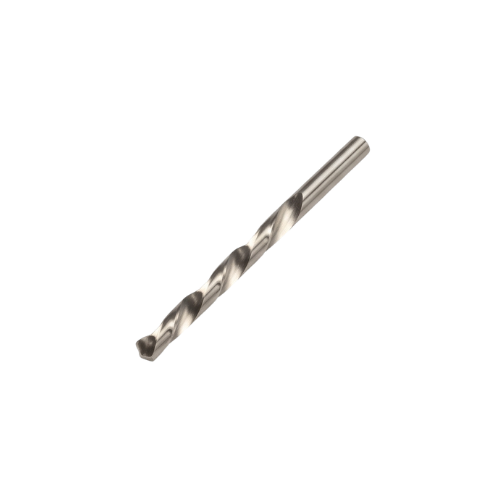
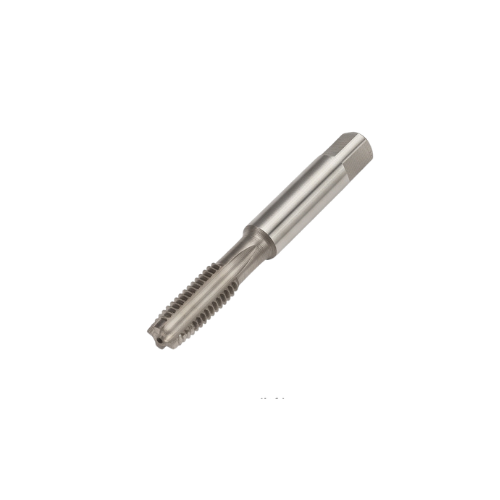
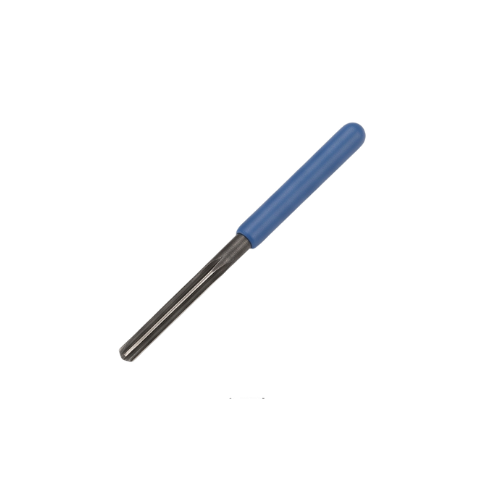
To use HeliCoil inserts, hole preparation is necessary. The basic principle is to create an “oversized” hole from the original one, such that there will be space for the thread insert to sit in, and lodge itself against the work piece. To prepare this hole effectively, we will need the following items.
 |
 |
 |
 |
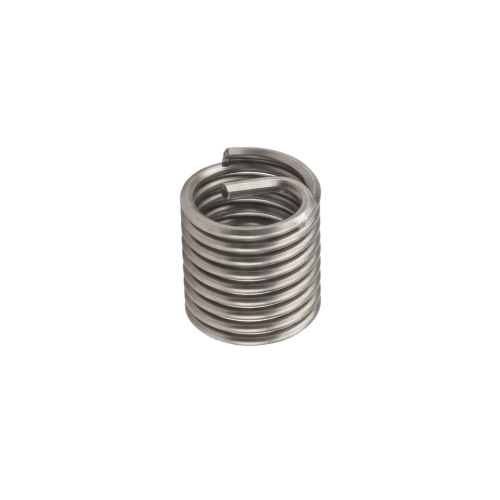 |
| 1. Drill bit | 2. Screw Thread Insert Tap | 3. Installation Tool | 4. Tang Break-off Tool | 5. Helical Insert |
Section D: HeliCoil Thread Insert Repair Process
The process of helical thread installation involves 4 major steps. They are listed chronologically below.
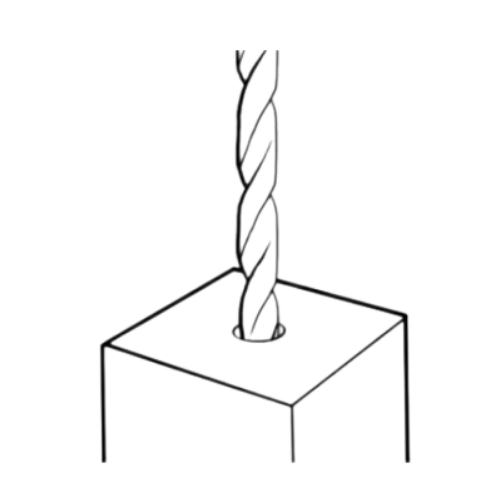 |
Drill
The main purpose of drilling is to enlarge the hole. Drilling is also used to clear out damaged threads (if necessary). |
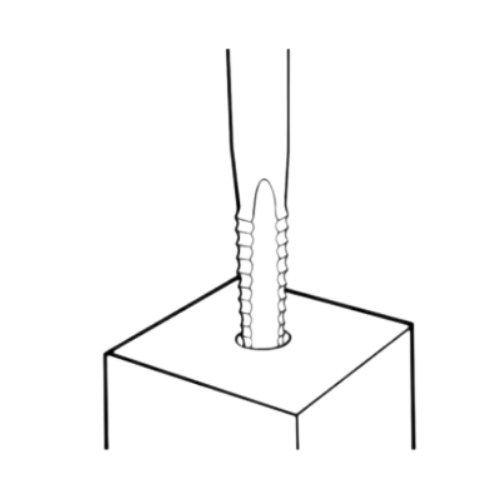 |
Tap
Re-tap the hole using the Screw Thread Insert (STI) tap. Tapped threads should match those on the bolt perfectly. |
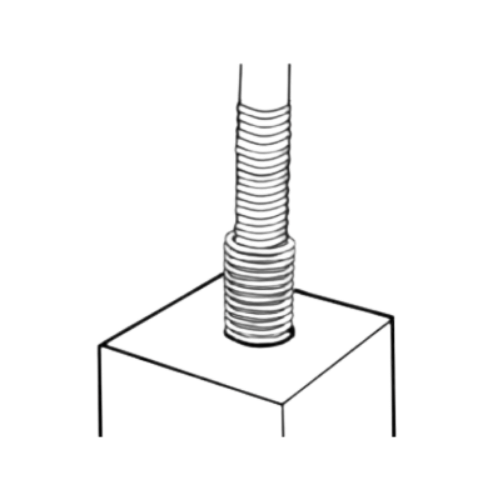 |
Install
With collar flush to the insert, wind the helical insert in using the inserting tool with light downward pressure until the insert is 1/2 to 1 coil below the surface, driving the tang towards the bottom of the hole. |
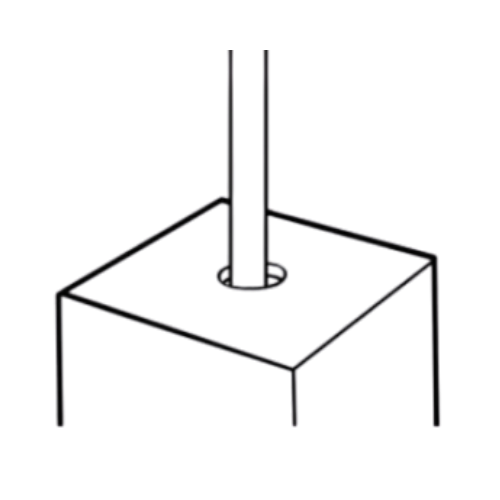 |
Tang Removal
Put the tang break-off tool into the insert and give it a light tap with a hammer to break the tang off. Note: for larger sized inserts, use long nose pliers to break the tang off. |
Section E: Helical Thread Insert Repair Process – Drilling
|
Drill
The main purpose of drilling is to enlarge the hole. Drilling is also used to clear out damaged threads (if necessary). |
For hole preparation, the drill size must follow those given by the HeliCoil manufacturer*. Any incorrect drill size used may lead to over or under enlargement of the hole, that subsequently causes the insert to not sit properly during installation.
*For screw thread inserts that differ in brand, every manufacturer of screw thread inserts follows a different set of drill sizes to fit their own inserts. It is therefore, recommended that you stick to the recommendation given by a brand of inserts and not inter-change drills and taps.
Section F: HeliCoil Insert Repair Process – Tapping
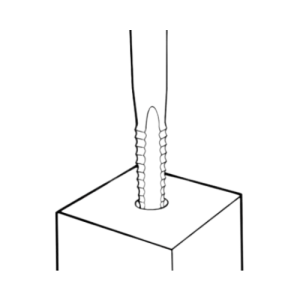 |
Tap
Re-tap the hole using the Screw Thread Insert (STI) tap. Tapped threads should match those on the bolt perfectly. |
Different types of taps
HeliCoil taps follow the same configuration of standard taps. Namely, they are available in 5 different designs:
- Roughing (also known as No.1)
- Finishing (also known as No.2)
- Bottoming (also known as No.3)
- Spiral Point
- Spiral Flute
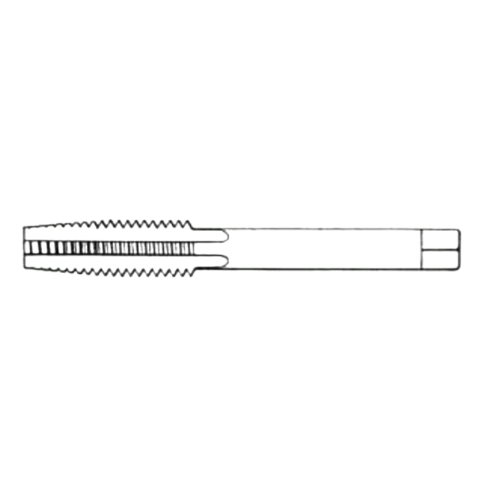 Roughing Taps |
Also known as Taper taps, they have a 4 thread chamfer, and are made undersize to reduce the load on finishing taps. Roughing taps are used for difficult tapping operations. |
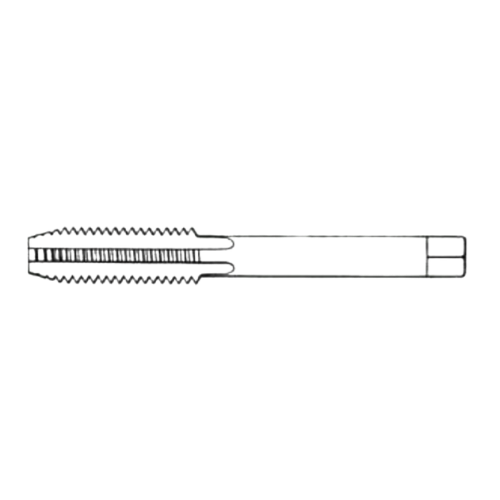 Finishing Taps |
Also known as Intermediate taps, they have a 4 thread chamfer, and are used for hand or machine tapping in through holes or blind holes where ample chip clearance is available. |
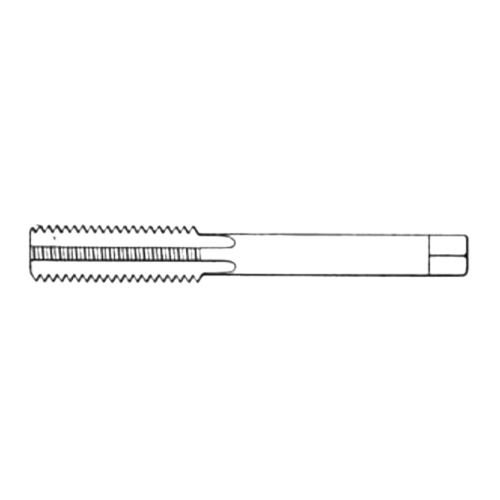 Bottoming Taps |
Also known as Plug taps, they have a 2 thread chamfer, and are used for tapping blind holes where a maximum number of fully-formed threads are needed in minimum depth holes. |
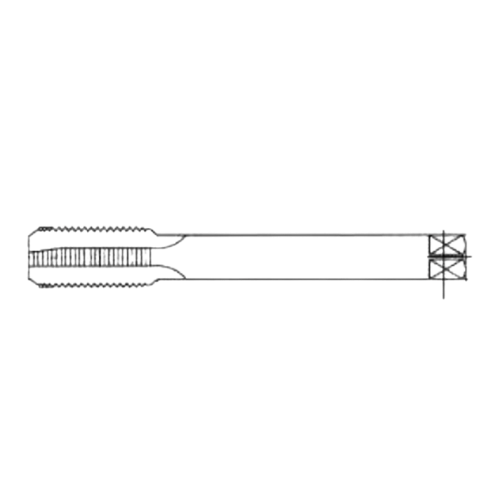 Spiral Point Taps |
Spiral Point taps have a 2 thread chamfer, and are used for through holes on less abrasive materials. They incorporate an angular grind at the point end which shears chips and drives the swarf forward. They are recommended for use in through holes or blind holes where ample chip clearance is available. |
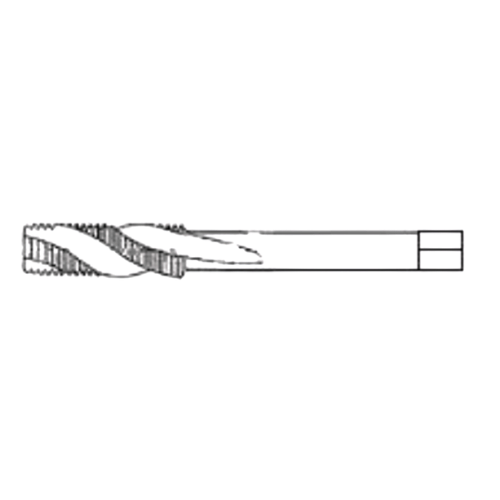 Spiral Flute Taps |
Spiral Flute taps can be used manually or attached to tapping drivers. They are specially designed for efficient removal of stringy chips out of deep or blind holes in soft materials. Spiral Flute machine taps directs the swarf backwards out of the hole. |
Section G: HeliCoil Insert Repair Process – Installation
Installation of HeliCoil inserts follows a simple principle: driving the insert using the tang. Depending on various factors such as speed, volume and ease of installation, there are many tools that can achieve these purposes. For a basic understanding, we will look at the simplest tool, which is a HeliCoil mandrel.
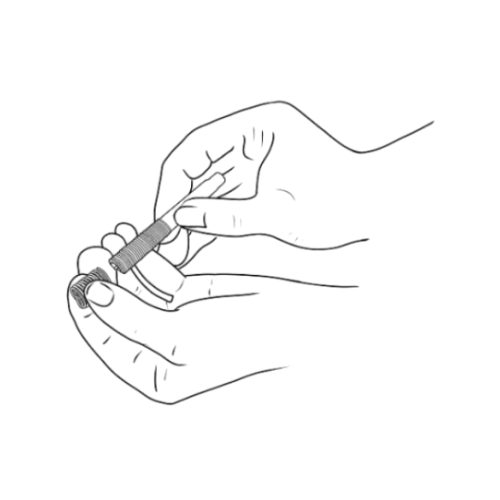 |
Loading
Using your hands, load the insert onto the mandrel by screwing it in. At the point where the insert cannot be turned anymore, the notch should meet the drive of the mandrel. |
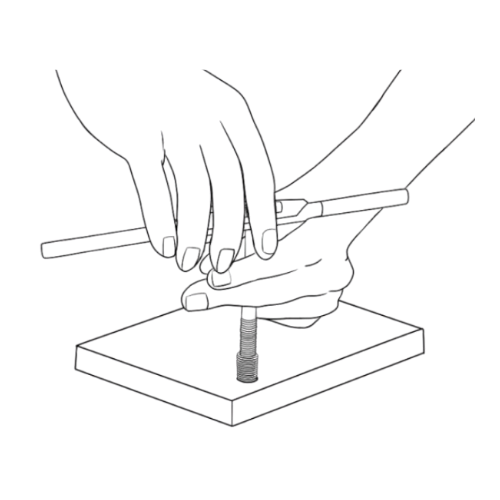 |
Aligning
For ease of installation, do use a tap wrench. Try and align the mandrel such that it is perpendicular to the work piece. |
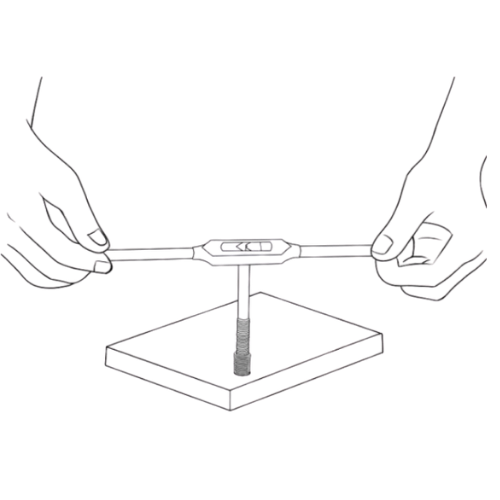 |
Driving
Wind the helical insert in using the mandrel with light downward pressure until the insert is 1/2 to 1 coil below the surface, driving the tang towards the bottom of the hole. |
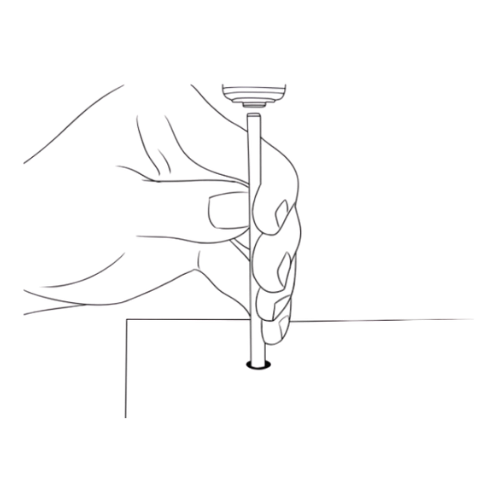 |
Breaking the tang
Finish the installation process by breaking off the tang with a tang break-off tool that is of the correct diameter. |
Troubleshooting
In the course of using HeliCoil inserts, there are some important points we need to take note of to ensure smooth installation. Below, we list some common mistakes that occur and the steps to take in order to prevent them.
- When tapping, the tap breaks.
Corrective action: Check that the hole is drilled to the correct diameter. Do not use drill bits that are worn as they may be undersized*. Also, always use tapping oil or lubricant when tapping.
*Just because a drill or tap is printed with a certain size, does not mean that the size will always be what is indicated (unless they are new). It is always critical to verify used drill bits and taps. For a rough reference, drill bits and taps will always wear considerably after usage for approximately 200 holes.
- While installing, the insert is not able to enter the threaded hole.
Corrective action: Make sure that the hole is drilled and tapped to the correct diameter* and tolerance. Use a STI (screw thread insert) gauge if possible. When installing, make sure the insert is held in place by the collar and sits vertically on the hole before turning in.
For screw-lock inserts, it is important to use prewinder-type tools, as the hexagon coil needs to be compressed before it can enter the tapped hole.
*Interchangeability is important. Make sure the brand of inserts used corresponds to the tap. Generic taps made by tap manufacturers who do not produce HeliCoil inserts may not match.
- After installation, the coil does not sit properly on the tapped hole, and one (or more) of the threads “jumps”. As a result, the screw may not be fastened into the threaded hole.
Corrective action: Check that the hole is tapped properly, and that while installing, do not press down on the inserting tool. Use horizontal action to install the helical insert. For a more secure and smooth installation, use prewinder-type installation tools.
- When breaking the tang off, it does not break fully, but is bent at an angle.
Corrective action: Check to make sure that the hole is deep enough for the tang to be completely broken off (there should enough space for the tang to bend 90⁰).
- After the tang is broken off, the screw cannot be fastened beyond the last thread. That is, when it reaches the bottom thread, it gets stuck.
Corrective action: Check that the last thread did not “jump”, as it could have been pulled downwards when the tang was broken off. Always use enough, but not too much force when breaking the tang off. Use an automatic spring-loaded tang break-off tool if possible.
Frequently Asked Questions (FAQ)
- The insert, in its free state, does not fit ‘snuggly’ into the screw, but is bigger than the screw. Is this normal?
Answer: Yes, this is normal. The HeliCoil insert in its free state is always ‘oversized’, compared to the threaded hole. This is so that after installation, the insert is able to exert radial pressure and lodge itself against the work piece.
- A certain thread insert has a nominal length of 10 mm as stated in the specifications table. However, when I measured the actual insert, it only shows 7 to 8 mm. At other times, it may even show only 5 to 6 mm. Is this correct?
Answer: Yes, this is normal. Due to wire tension, a thread insert may be more ‘compressed’ (where the coils stay close together) or ‘open’ (the coils stay further apart from each other). They should not be measured in their free state, and will reach their stated nominal lengths after they have been installed, as they will then follow the tapped thread dimensions.
- After the insert is installed, I checked the hole using a standard thread plug gauge. However, the No-Go side enters freely while sometimes, the Go side does not enter at all. Is this normal?
Answer: Yes, this is normal. Because the HeliCoil insert is made with a rhombus cross-section, this may differ from the angle of the standard gauge. Therefore, it is not necessary, and in fact, wrong to check the hole with a helical insert with a standard gauge. For checking, use a STI gauge before installing the threaded insert.
- What length of insert should I use?
To determine which length to use, it is important to refer to the drilling and tapping depths chart (typically denoted by our symbols “Q”, “R”, “S” and “T”). They will tell you the effective thread engagement for every insert length.
- What are Screw Lock inserts?
In addition to all the characteristics of the Free Running insert, Screw Lock inserts have one or more of its intermediate coils deformed polygonally. This serves to create strong resilient pressure onto the thread flanks of the bolt as it passes through.
- What is the purpose of Screw Lock inserts?
The built-in Prevailing Torque of the grip coil positively locks the bolt, safeguarding against loosening under vibration or impact.
- Why does my screw not enter freely into a hole that has a screw lock insert installed?
This is because our fingers do not provide sufficient force in fastening the screw. For correct installation, the initial threads can be fastened by hand. When the screw reaches the grip coil, you must use a driver (whether it be an Allen key or Philips screwdriver, depending on your screw) to fasten further.
- Why are there so many types of HeliCoil inserts?
Technically, HeliCoil is a brand, so there is only one type of HeliCoil Insert. There are many types of screw thread inserts in the market, but they are known by different brand names.
- Why is HeliCoil available from different manufacturers?
Originally, HeliCoil was invented and produced by Emhart Teknologies (known today as Stanley Engineered Fastening) from the USA in 1938. Till today, they are the only company in the USA to produce HeliCoil inserts.
Outside of USA, Bollhoff GmbH from Germany and Bollhoff Armstrong Ltd from the United Kingdom are the only companies licensed to produce HeliCoil inserts and tools.
- Are all these HeliCoil inserts the same?
As long as an insert is produced from any of these companies, they conform to the same stringent and quality-assured standards. Unless special manufacturing instructions are given, their dimensions are all the same.
- HeliCoil inserts produced from all 3 companies carry different part numbers. Why is this so?
As every company has its own accounting system, their references to HeliCoil inserts and tools also change. However, official letters and Certificates of Conformity (COC) can be issued to verify the inter-changeability across all items.
- Why are some stainless steel HeliCoil inserts darker in shade than others?
HeliCoil inserts are derived from stainless steel raw materials, which may be darker or lighter in shade. However, all HeliCoil undergo a passivation process before being delivered. Depending on the origin of these raw materials, HeliCoil inserts may take the colour as well.
- I noticed that some HeliCoil inserts are longer than others, even though they have the same nominal length. Correspondingly, the longer inserts have a wider gap between coils. Why is this so?
Being cold-rolled from stainless steel wires, HeliCoil inserts tend to have some spring-like properties, which may result in inserts being more “compressed” or “open”, thus appearing longer than others. This is not to be taken as the correct length of the insert, as the length is ultimately realized after the insert has been installed inside the threaded hole. A more accurate reading and verification of the length is to check the number of coils on the insert, which is given in our catalogue table.


10 Ubi Crescent #01-80 Lobby E, 408564, Singapore

(65) 6743 4155

(65) 6743 4155

sales@thorintl.com

Mon - Fri: 9am - 5pm
Sat - Sun: Closed

MRT
Take the appropriate MRT line to the nearest station, then continue your journey by bus, walking, or a taxi/ride-hailing service.

Bus
Check the bus services near the company’s location, board the relevant bus, alight at the nearest stop, and walk a short distance to the office.